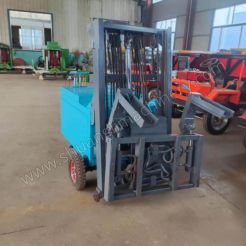
Pendulum bucket elevator conveyor
Overview:The Pendulum Bucket Elevator Conveyor is a high-performance material handling solution designed for various industries, including food processing, pharmaceuticals, and manufacturing
Product Description
Pendulum Bucket Elevator Conveyor Product Description
Overview:The Pendulum Bucket Elevator Conveyor is a high-performance material handling solution designed for various industries, including food processing, pharmaceuticals, and manufacturing. This innovative conveyor system is engineered to move bulk materials efficiently and reliably, ensuring maximum productivity and minimal downtime.
You will get efficient and thoughtful service from Jinghang.
Key Specifications:
- Material: Constructed from high-quality stainless steel and durable polymers, guaranteeing resistance to corrosion and wear.
- Size: Customized lengths available from 10 to 50 meters, with bucket sizes ranging from 5 to 100 liters.
- Capacity: Accommodates up to 1500 kg per hour, depending on the configuration.
- Weight: Lightweight design enhances ease of installation and minimizes structural requirements.
Unique Features:
- Advanced Pendulum Design: Ensures gentle handling of materials, preventing damage while maximizing loading capacity.
- Modular Construction: Facilitates easy expansion or reconfiguration to meet evolving operational demands.
- AI Integration: Equipped with smart monitoring systems that provide real-time data on performance metrics and maintenance alerts.
- Adjustable Speed Options: Allows for fine-tuning of operation speed based on material characteristics and throughput requirements.
Performance Attributes:
- High Efficiency: Optimized design enables smooth material flow, significantly reducing energy consumption.
- Rapid Operation: Capable of operating at speeds up to 60 meters per minute, ensuring quick transfer of materials.
- Robust Load Capacity: Supports a diverse range of materials—from grains to powders—safely and efficiently.
Problem-Solving Capabilities:The Pendulum Bucket Elevator Conveyor addresses common challenges faced in material handling. Its gentle yet effective design minimizes product breakage and degradation, which is crucial for fragile items in the food and pharmaceutical sectors. The smart monitoring system enhances operational efficiency and reduces maintenance costs by predicting failures before they occur, directly improving productivity and extending equipment lifespan.
This elevator conveyor is a reliable investment for businesses looking to enhance their material handling operations, streamline workflow, and ultimately increase profitability. Discover the difference with our Pendulum Bucket Elevator Conveyor.
Related Products:Pendulum bucket elevator conveyor, straight-line Pendulum bucket conveyor